Inconsistent bearing quality across batches usually stems from raw material shifts, process drift, or inspection gaps. Diagnose symptoms like noise or dimensional drift, verify supplier quality control records, and use defect analysis to trace the root cause. Standardize incoming checks to prevent recurrence.
- Batch variation often appears as noise, dimensional drift, or fit issues that only show up after assembly.
- Supplier quality control records, not just certificates, reveal whether the control system is functioning.
- Defect analysis requires correlating test data with production logs from the specific batch.
- Incoming inspection must check the same parameters that caused the failure in the field.
- Documented corrective action from the supplier is the only reliable way to stop recurrence.
Why one supplier delivers different quality in different batches
Bearing quality inconsistency rarely appears as a single, obvious failure. It shows up slowly. One lot runs quiet for three months. The next lot introduces a faint hum at operating speed. The lot after that causes premature spalling on the outer race. Engineers often assume the bearing design changed, the application changed, or the installation changed. In many cases, the application stayed the same, and the bearing changed.
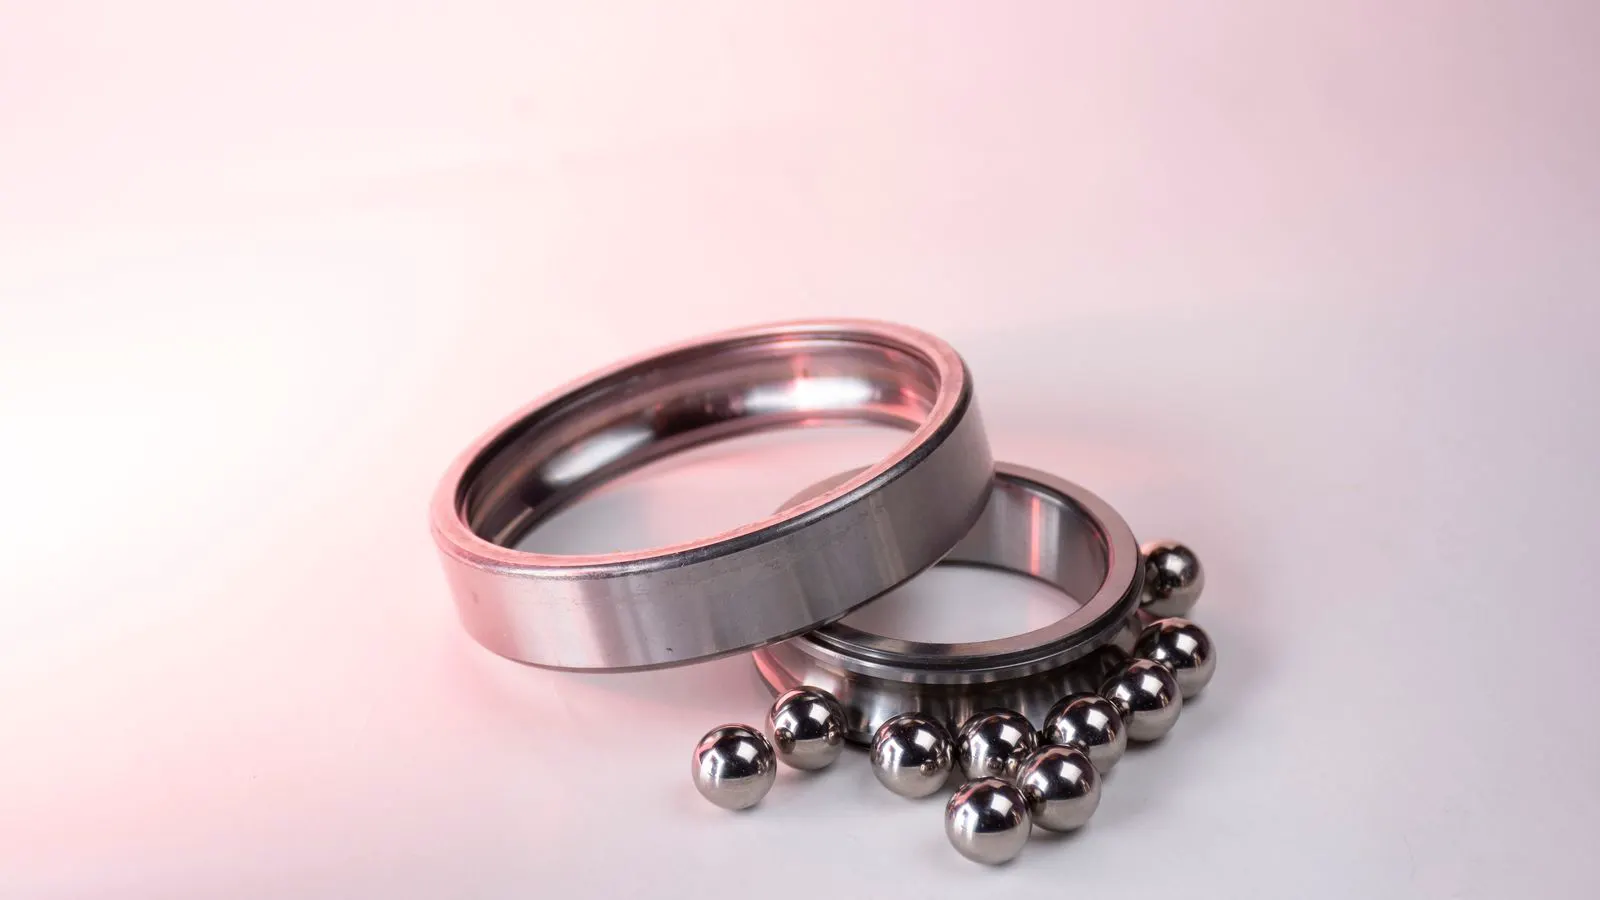
This happens because a bearing is not a single manufactured part. It is a system of components. The steel, the grease, the race geometry, the rolling element dimensions, and the final assembly process all interact. When one element shifts outside its intended tolerance, the whole system behaves differently. If the supplier does not tightly control each of these elements, batch variation becomes unavoidable.
The problem becomes more difficult when the supplier is consistent in paperwork but inconsistent in execution. A supplier can provide a certificate of conformity for every batch and still deliver parts that perform differently. The certificate confirms the batch passed their defined tests at that moment. It does not guarantee the batch will behave identically to the previous batch under your operating conditions.
Common symptoms of batch variation
Before diagnosing a root cause, you must identify the symptom. The same underlying process drift can manifest in several ways depending on the application. A table helps map these symptoms to likely causes.
| Symptom | Likely cause | What to do |
- Intermittent noise or vibration at specific RPM
| Raw material hardness variation or rolling element geometry drift
| Request raw material test reports for the specific heat lot. Check if the noise frequency matches bearing geometry - Dimensional drift in bore or OD after heat treatment
| Furnace control drift or quench oil contamination
| Measure critical dimensions on incoming stock. Require process control records from the heat treatment stage - Inconsistent grease performance or early contamination ingress
| Grease batch inconsistency or seal assembly variation
| Check grease fill volume and seal compression on received parts. Compare grease viscosity between batches - Premature spalling on raceways
| Surface finish degradation or insufficient peening
| Inspect surface roughness and peening parameters. Request surface finish certificates for the specific batch - Uneven rolling element spacing or wobble
| Assembly process drift or lack of final inspection
| Perform dimensional and runout checks on incoming bearings. Request final assembly inspection records - Inconsistent fit with shaft or housing
| Hardness variation causing dimensional instability
| Measure bore and OD dimensions. Check hardness certificates and compare across batches
Noise is often the first visible sign, but dimensional drift is usually the first measurable sign. If you have a CMM or precision micrometers, measure dimensions before assembly. If you do not, listen. A bearing that sounds different from the previous batch is a bearing that will likely fail differently.
How to verify supplier quality control records
A supplier quality control system is only as good as its records. Do not rely on the existence of an ISO 9001 certificate. A certificate confirms the system was audited at a point in time. It does not confirm the system is functioning now.
Ask for the process control records for the specific batch you received. These records should show:
- Raw material heat lot number and test reports
- Dimensional measurement logs for critical features
- Surface finish measurements
- Hardness test results
- Final assembly inspection data
- Grease fill volume and seal test results
If the supplier cannot provide these records for the specific batch, the control system is not functioning as it should be. A supplier that can provide aggregate data but not batch-specific data is hiding variation. A supplier that provides batch-specific data but cannot explain deviations is not controlling the process.
When reviewing these records, look for trends, not just pass/fail status. A dimension that passes every single check but drifts upward over ten batches is a problem. The control system is reacting to the data, but the process is not stable. Ask the supplier to show their control charts. If they do not maintain control charts, they are managing by inspection, not by process control.
Running defect analysis on failed or suspect bearings
When a batch fails, the defect analysis must be specific. Do not send a single failed bearing and ask for a general explanation. Send the failed bearing and the control records for that batch.
The analysis should follow a logical path. First, identify the defect type. Is it spalling, pitting, fatigue, or mechanical damage? Second, locate the defect. Is it on the inner race, outer race, rolling elements, or in the lubricant? Third, correlate the defect location with the defect type. Spalling on the inner race near the rolling element contact point suggests fatigue. Spalling on the outer race suggests contamination or impact.
Next, compare the defect pattern to the control records. If the defect is related to surface finish, check the surface roughness data for that batch. If the defect is related to hardness, check the hardness data. If the defect is related to grease, check the grease fill data.
If the supplier cannot correlate the defect to a process parameter, the analysis is incomplete. A useful supplier will identify which process step likely allowed the variation to occur. They will also propose a corrective action. This corrective action must be specific. It must not be a general statement like “we will pay more attention.” It must be a change to a process parameter, a new measurement point, or a revised specification.
Standardizing incoming inspection to catch variation early
The best way to manage bearing quality inconsistency is to catch variation before it reaches your assembly line. This requires a standardized incoming inspection protocol.
The protocol should include:
- Visual inspection for contamination, damage, or missing parts
- Dimensional measurement of bore, OD, and width
- Hardness verification where applicable
- Noise or vibration test where the equipment is available
- Review of supplier quality control records for the specific batch
The key is consistency. Do not inspect one batch thoroughly and another loosely. Do not inspect dimensions in one batch and skip them in another. The inspection protocol must be the same for every batch from every supplier.
When you find a variation, do not just reject the batch. Document the variation. Record the specific parameter that was out of spec. Record the magnitude of the deviation. Record the date and batch number. This data becomes your basis for corrective action requests.
A supplier that receives repeated, specific corrective action requests will eventually adjust their process. A supplier that receives vague complaints will not. The specificity of your incoming inspection data is what forces the supplier to address the root cause.
Managing the supplier relationship after identifying variation
Once you have identified a quality issue and received a corrective action, you must verify that the action works. Do not assume the next batch will be fine because the supplier said it would be.
Request the control records for the next three batches. Compare them to the previous batches. If the variation persists, the corrective action was not effective. Escalate the issue.
If the variation is significant, consider reducing the order quantity for that supplier. Place more orders with a second or third supplier. This creates competitive pressure and gives you more data to compare.
If the variation is minor but consistent, work with the supplier to adjust your specification. Sometimes the bearing is within its general tolerance but outside your application tolerance. A tighter specification on the critical dimension may be necessary. This requires a conversation with the supplier about their process capability. If they cannot meet your tightened specification, they cannot supply that bearing for your application.
The goal is not to punish the supplier. The goal is to stabilize the supply. A stable supply is worth more to you than a cheaper supply that requires constant troubleshooting.
Prevention tips for long-term quality stability
Prevention is cheaper than troubleshooting. The following practices reduce the risk of future issues.
- Require batch-specific quality control records for every order
- Perform incoming inspection on the same parameters every time
- Maintain a record of all batch variations and supplier responses
- Qualify at least two suppliers for critical bearings
- Review supplier process capability annually
- Include quality performance in supplier scorecards
- Communicate field failure data back to the supplier
The most effective prevention is data. Without data, you are guessing. With data, you are managing. A bearing supplier that receives clear, specific, and consistent data will improve their process. A bearing supplier that receives vague complaints will not.
Frequently asked questions
How do I know if a bearing quality issue is from the batch or from my installation?
Check the same bearing model from a different batch. If the new batch performs normally, the previous batch was defective. If the new batch also performs poorly, the issue is likely in your installation or application.
Can I trust a supplier certificate of conformity?
A certificate confirms the batch passed the supplier's defined tests. It does not guarantee the batch will perform identically to previous batches under your conditions. Request the underlying process control records to verify the data.
What is the minimum incoming inspection I should perform?
At minimum, perform visual inspection, dimensional measurement of critical features, and review of supplier quality control records. Add noise or vibration testing if your application is sensitive to performance.
How do I ask a supplier for corrective action without damaging the relationship?
Be specific and factual. Provide the batch number, the defect description, and the control records you reviewed. Ask for a root cause analysis and a specific corrective action plan. Avoid blame. Focus on the process.
When should I switch bearing suppliers?
Switch when the supplier cannot provide batch-specific control records, cannot identify the root cause of a defect, or cannot implement a corrective action that is verified by the next batches. A supplier that cannot manage variation will continue to create it.